
The Demanding Realities of Industrial Shredding and Cutting Tools
In modern recycling and waste-processing facilities, the fine line between profitability and expensive downtime is determined directly on the rotor of the industrial shredder. Whether processing automotive scrap, used tires, electronic scrap (WEEE), municipal solid waste (RDF/SRF), industrial plastics, or heavy cables, shredder knives operate under extreme tribological stress. They encounter continuous abrasive wear alongside severe mechanical shock loads caused by uncrushable tramp metals, stone contamination, and uneven feed rates.
Substandard blades compromise productivity immediately. They suffer from rapid edge blunting, edge micro-chipping, and catastrophic cross-sectional fracture. When a blade breaks off the rotor, it frequently damages the knife seats, counter-knives, rotor body, and sizing screens, resulting in thousands of euros in secondary repair costs and unplanned plant shutdowns. Achieving extended blade life and dependable continuous throughput requires two foundational pillars: matching the tool steel grade to the targeted waste stream and applying a specialized heat treatment protocol designed for high impact toughness.
Steel Selection: Balancing Wear Resistance and Impact Toughness
A persistent error in shredder blade specification is over-prioritizing surface hardness at the expense of core toughness. Hardening a standard alloy past 60 HRC might delay fine abrasive wear, but it transforms the blade into a brittle structure incapable of absorbing sudden mechanical deflection. When foreign tramp metal enters the shredding chamber, excessive brittleness causes immediate fracturing rather than controlled micro-wear. A reliable shredder knife demands high surface wear resistance to retain sharp cutting geometry, supported by high matrix toughness to endure violent impact forces without crack propagation.
The primary tool steel grades utilized in heavy-duty recycling applications include:
- AISI D2 / DIN 1.2379 (High-Carbon, High-Chromium Cold Work Steel): Formulated with 12% chromium and high carbon content, D2 provides abrasive wear resistance. It represents an industry standard for granulating clean plastics, film shredding, and controlled secondary processing. However, its primary carbide network yields moderate shock toughness; unmonitored feed streams containing heavy tramp metal can trigger premature chipping on cutting edges.
- DIN 1.2631 / Shock-Resisting Chipper Steels: Engineered with balanced additions of silicon, chromium, and molybdenum, this grade delivers shock absorption. It is the premier choice for primary shredders, tire recycling lines, and timber chipping drums. While its abrasive abrasion resistance is lower than D2, its resistance to structural fracturing under shock loading is exceptional.
- AISI H13 / DIN 1.2344 (Modified Hot Work Tool Steel): Recognized for structural stability under combined thermal and mechanical stresses. In high-friction shredding lines where cutting zones exceed 200°C—such as dense baled plastic or high-compression refuse shredding—H13 maintains structural integrity without thermal softening or micro-cracking.
- Powder Metallurgy (PM) Tool Steels (e.g., CPM / Vanadis Series): Produced via atomized powder consolidation rather than conventional ingot casting, PM steels eliminate coarse carbide segregation. The resulting ultra-fine, uniform carbide structure delivers a rare engineering combination: extreme abrasive wear resistance (60–62 HRC) paired with impact fracture toughness that surpasses conventional ingot steels. PM grades offer the lowest total cost of ownership for high-tonnage processing of abrasive composite scrap and glass-fiber reinforced plastics.
| Steel Grade | Typical Hardness | Impact Toughness | Wear Resistance | Primary Shredding Application |
|---|---|---|---|---|
| D2 (1.2379) | 56 – 60 HRC | Moderate | Very High | Plastic Granulation, Cable Stripping, Film |
| 1.2631 | 53 – 56 HRC | Very High | Moderate / Good | Primary Pre-Shredders, Scrap Tires, Wood |
| H13 (1.2344 Mod.) | 50 – 54 HRC | Superior | Moderate | High-Thermal Friction Shredding, Dense RDF |
| PM Tool Steels | 58 – 62 HRC | High | Exceptional | E-Waste, Abrasive Composites, Continuous Lines |
Advanced Heat Treatment: Engineering the Core Matrix
Sourcing premium tool steel is only half the battle; improper thermal processing will degrade even the highest alloy. Optimizing shredder blades for maximum impact resistance demands a controlled multi-stage heat treatment process:
- Vacuum Austenitizing with High-Pressure Gas Quenching: Heating blades in automated vacuum furnaces prevents surface decarburization, oxidation, and scaling. Controlled, uniform heating ensures that core and surface sections reach structural equilibrium simultaneously, minimizing residual internal stresses and distortion prior to quenching.
- Sub-Zero Cryogenic Treatment: During initial quenching, a fraction of unstable austenite fails to transform, remaining trapped within the steel matrix as "retained austenite." By exposing the blades to deep cryogenic temperatures between -140°C and -196°C, retained austenite is converted into stable, wear-resistant martensite, eliminating long-term dimensional drift and latent micro-cracking.
- Multi-Stage Tempering: Impact-loaded blades must never rely on single-cycle tempering. Applying two to three successive precision tempering cycles relieves micro-stresses created during quenching, fine-tunes target hardness, and maximizes fracture toughness across the entire blade cross-section.
Frequently Asked Questions (FAQ)
Why do industrial shredder blades crack and fracture during operation?Premature blade fracturing is primarily caused by an imbalance between material hardness and shock toughness, often exacerbated by using excessive hardness (>60 HRC) on inhomogeneous waste streams. If uncrushable tramp metals or stones enter the chamber, a brittle blade cannot flex or absorb the kinetic shock, leading to catastrophic failure. Selecting high-toughness steel grades and performing multi-stage vacuum tempering resolves this issue.
Is AISI D2 (1.2379) steel always the best choice for shredder knives?No. While D2 is widely used due to its wear resistance in clean plastics, films, and copper cables, its coarse carbide network leaves it vulnerable to edge chipping under heavy mechanical impact. For primary shredders processing municipal waste, scrap tires, or mixed post-consumer waste, shock-resistant alloys such as DIN 1.2631 or modified hot-work steels provide significantly higher structural reliability.
Are physical vapor deposition (PVD) surface coatings recommended for shredder knives?In primary recycling applications with severe impact shocks, thin surface coatings (such as TiN or TiAlN) often delaminate rapidly under heavy mechanical abrasion and substrate deflection. Rather than relying on superficial thin-film coatings, facilities achieve far better return on investment by selecting homogeneous Powder Metallurgy (PM) steels or deep cryogenic vacuum treatments that enhance the structural properties throughout the entire volume of the blade.
What maintenance procedures best prevent unplanned blade failures?Preventive maintenance requires consistent inspection of cutting clearances between rotor and stator knives, strict monitoring of torque tolerances on mounting bolts, and regular re-sharpening before edge rounding exceeds safe thresholds. Operating severely rounded blades increases motor amperage, induces excessive thermal stress, and accelerates shock-induced cracking across the rotor assembly.
Maximize Your Uptime with Snijer Engineering
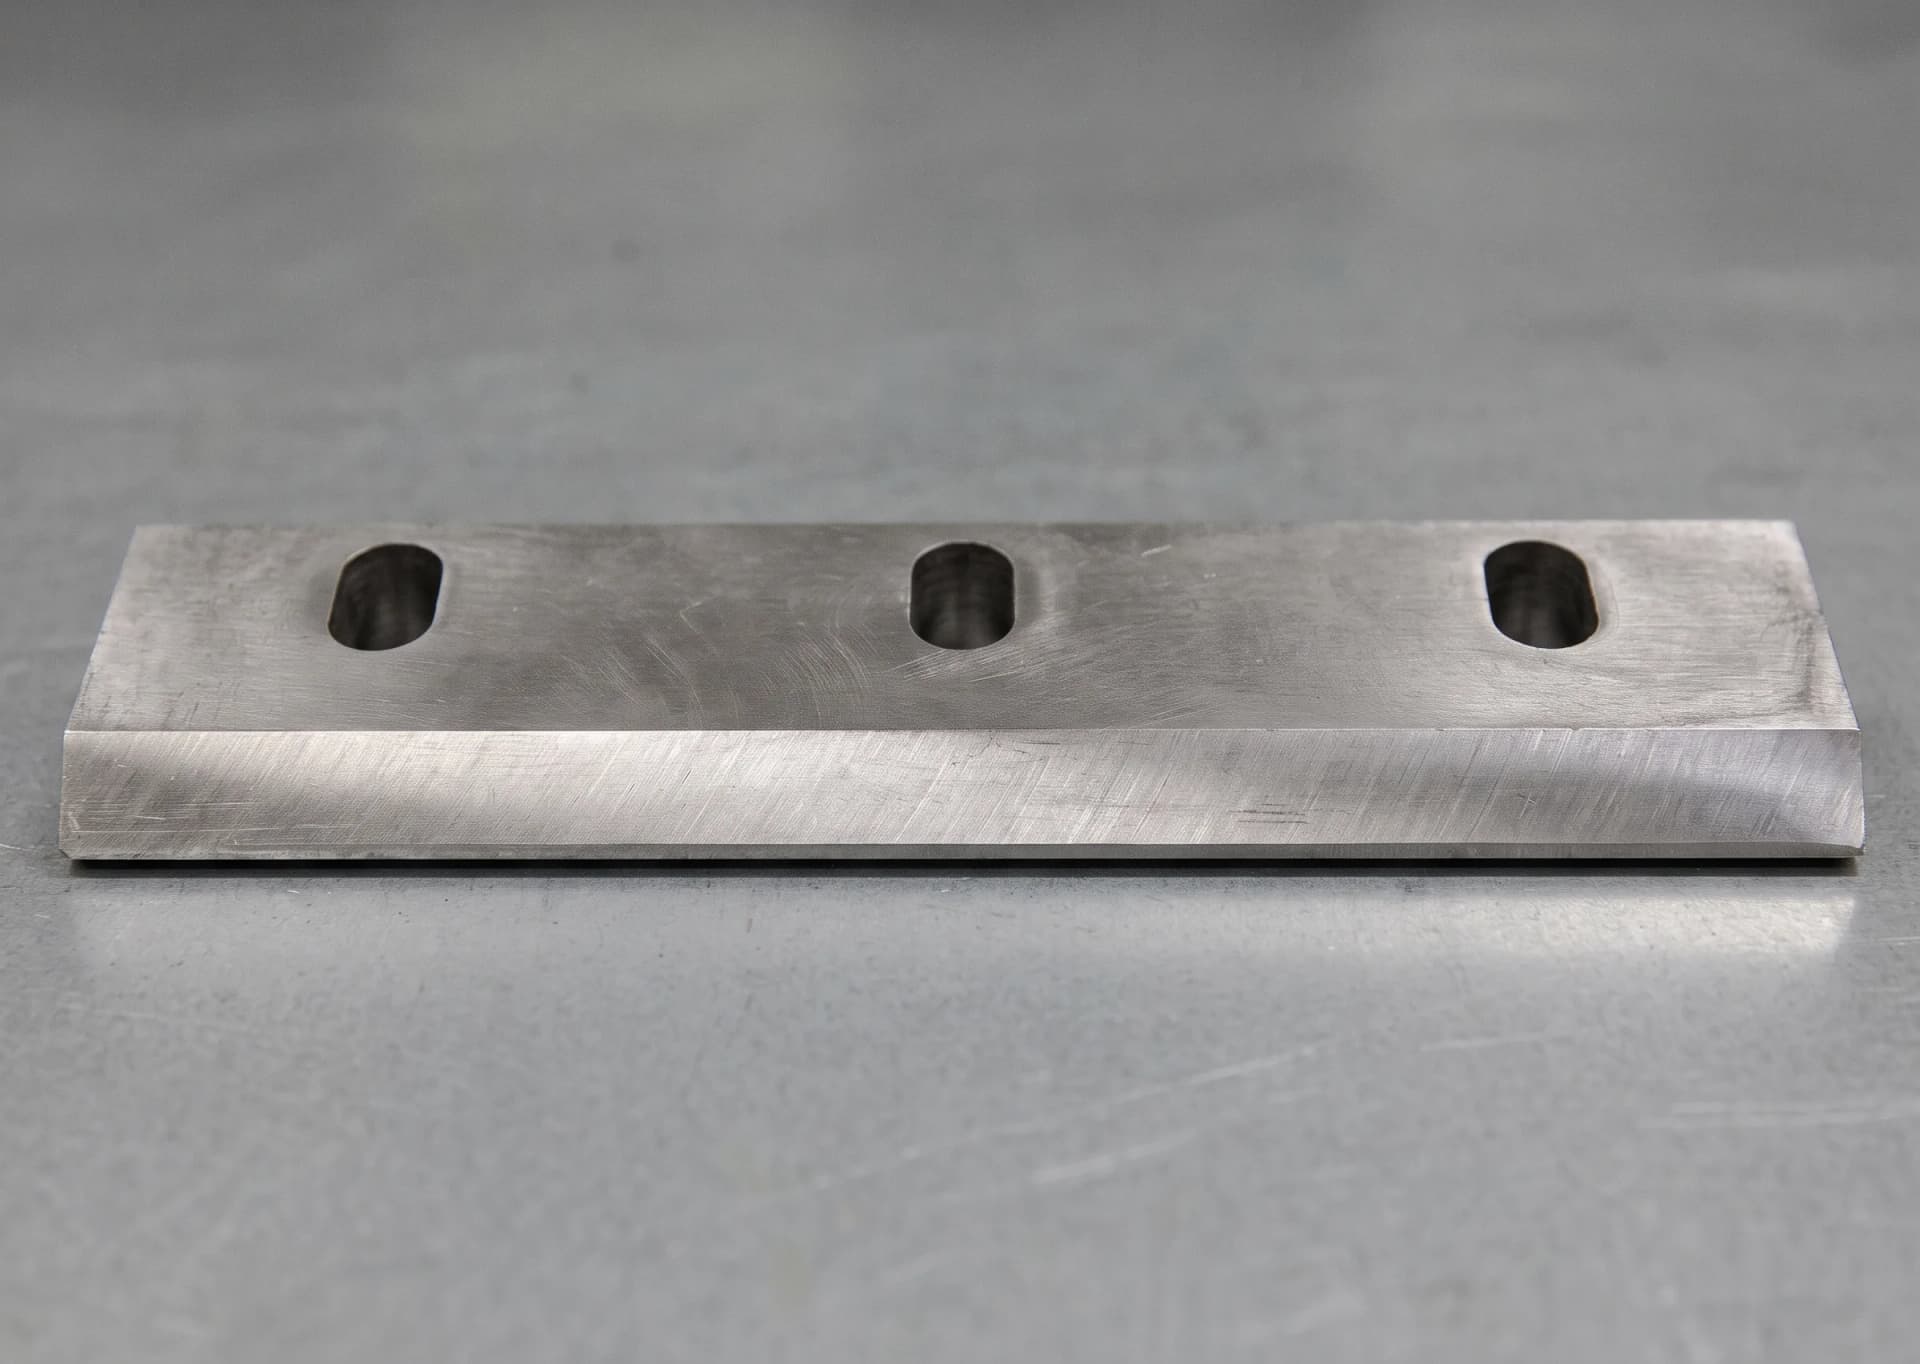
Snijer analyzes down-to-the-minute operational data from recycling plants globally to engineer industrial knives that conquer abrasive wear and mechanical shock. We manufacture customized, high-precision shredder and granulator knives compatible with major European and global shredder platforms (including Lindner, Untha, Weima, Eldan, Zerma, and Vecoplan). From tailored alloy selection to precision CNC grinding and cryogenic vacuum hardening, our components lower total cost of ownership. To eliminate unplanned downtime and receive an engineered cutting tool consultation, please contact the Snijer engineering team today.